
Featured Industrial & Specialty Chemical Products
Custom-compounded chemical concentrates and eco-certified surfactants engineered for commercial cleaning suppliers, industrial buyers, and private label distributors across Australia.
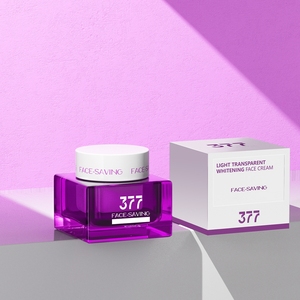
OEM Anti Aging Hydrolyzed Collagen Hyaluronic Acid Cream Arbutin Moisturizing Lightening Brightening Face Cream
Deep-moisturizing specialized dermal barrier formulation. High-stability emulsification ideal for commercial skin protection & healthcare facilities.
Inquire Now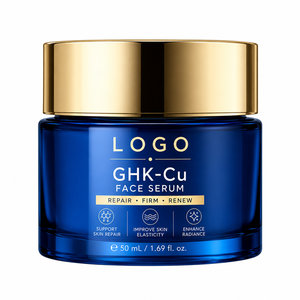
Private Label GHK-Cu Copper Peptide Face Cream Moisturizing Soothing Repair Anti-Wrinkle Firming Cream for All Skin Types OEM
Advanced bio-active copper peptide complex. Concentrated cell-repair matrix engineered for private label wellness and industrial safety lines.
Inquire Now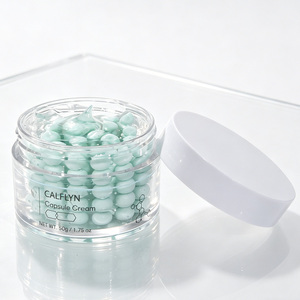
Capsule Pearl Ball Cream OEM ODM Private Label Collagen Anti-Aging Brightening Acne Control Hydrating Oil-Control Face Cream
Micro-encapsulated active release technology. Prevents oxidation of key functional ingredients for extended shelf-life in harsh Australian climates.
Inquire Now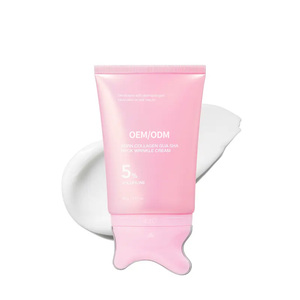
Private Label PDRN Collagen Gua Sha Neck Cream Cosmetic Tube Tighten Lift Neck Cream Volufiline 5 Anti Aging Wrinkle Cream 90g
Precision-dispensing tube package with localized targeted applicator. Formulated with cell-regenerative PDRN & premium lipid complexes.
Inquire Now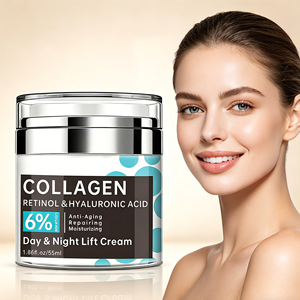
Private Label Collagen Retinol Hyaluronic Acid 7% Deep Moisture Nourishment Science Proven Formula Cream Skin Care Face Cream
Science-proven multi-active hydration complex featuring 7% hyaluronic system for heavy-duty barrier protection and deep tissue repair.
Inquire Now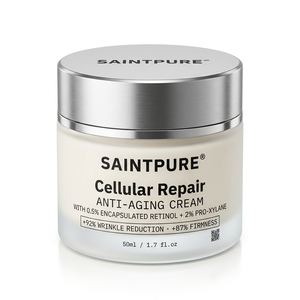
Private Label Anti-Aging Face Cream 50ml Encapsulated for Pro-Xylane Wrinkle Firming Cellular Repair Moisturizer OEM
Encapsulated Pro-Xylane delivery mechanism ensuring maximum bioavailability and structural stability under varied environmental conditions.
Inquire Now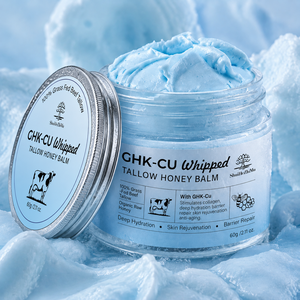
Private Label Copper Peptide GHK-Cu 100% Grass-Fed Beef Tallow Balm Deep Moisturizing Face Cream Anti-Aging Skin Repair OEM ODM
Heavy-duty natural lipid balm blend combining 100% grass-fed tallow with pure GHK-Cu peptides for intense barrier defense and extreme weather skin repair.
Inquire Now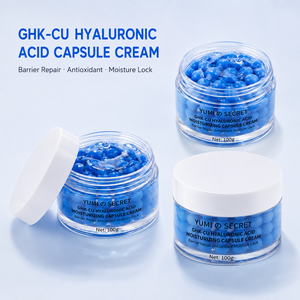
Private Label OEM GHK-Cu Copper Peptide Capsule Face Cream Anti Aging Firming Moisturizer for Mature Skin 100ml
Premix active capsule system suspended in an ultra-hydrating matrix. Provides extended active delivery for high-performance commercial lines.
Inquire NowNavigating Australia's Industrial Chemical Landscape: Regulatory Rigor & Eco-Surfactant Evolution
As Australia's industrial, agricultural, and commercial sectors undergo a decisive transition toward environmental sustainability and strict occupational health standards, the demand for high-performance, compliant industrial cleaning chemical formulations has reached an unprecedented peak. Importers, commercial cleaning brands, and industrial distributors across New South Wales, Victoria, Queensland, and Western Australia are challenged to balance aggressive degreasing efficacy with non-negotiable regulatory frameworks.
Navigating chemical importation into Australia requires strict adherence to the Australian Industrial Chemicals Introduction Scheme (AICIS), governed by the Department of Health and Aged Care. Any chemical introduction—whether raw surfactants, concentrated degreasers, institutional sanitizers, or specialized industrial barrier creams—must strictly comply with CAS inventory status, ecotoxicity thresholds, and Work Health and Safety (WHS) Regulations mandating Globally Harmonized System (GHS) Revision 7 Safety Data Sheets (SDS) and labeling.
AICIS Chemical Compliance
Full audit alignment with Australia's Inventory of Industrial Chemicals. Every single ingredient in our export compounding is pre-vetted for seamless Australian importation without registration bottlenecks.
GHS Revision 7 SDS & Labels
Complete preparation of Safe Work Australia-compliant GHS 7 Safety Data Sheets, correct signal words, hazard statements, precautionary statements, and emergency contact integration.
AS 4351 Biodegradability
Formulated using non-ionic and anionic surfactant systems tested to achieve >90% ultimate aerobic biodegradability under Australian Standard AS 4351 and OECD 301 testing guidelines.
Custom Chemical Synthesis & OEM Contract Compounding Capabilities
Our state-of-the-art manufacturing infrastructure in China operates fully certified ISO 9001:2015, ISO 14001:2015, and GMP (Good Manufacturing Practice) facilities equipped with high-shear emulsification reactors, automated multi-head liquid filling lines, and real-time analytical chromatography labs. We provide complete OEM/ODM solutions ranging from concentrated industrial degreasers and vehicle wash systems to commercial facility hygiene products and protective skin barriering creams.
| Chemical Category | Key Active Compounds | Australian Industry Application | Environmental / Safety Standard | OEM Customization Scope |
|---|---|---|---|---|
| Heavy-Duty Degreasers | Ethoxylated Alcohol, Sodium Metasilicate, D-Limonene, Eco-Solvents | Mining machinery (Pilbara), heavy transport workshops, marine engines | PFAS-Free, Quick-Break (AS 4351), Phosphate-Free | pH adjustment (11.0 - 13.5), dye addition, high-dilution ratios (up to 1:100) |
| Food Grade Sanitizers | Benzalkonium Chloride (QUAT), Hydrogen Peroxide, Peracetic Acid | Meat processing plants (Victoria/NSW), abattoirs, commercial kitchens | HACCP Australia compliant, FSANZ standard safe | No-rinse formulations, fragrance-free options, foaming vs non-foaming |
| Commercial Facility Cleaners | Alkylate Polyglucoside (APG), Citric Acid, Lauryl Glucoside | Hospitality, office towers (Sydney/Melbourne), institutional janitorial | GECA (Good Environmental Choice Australia) alignable | Natural essential oils, neutral pH (6.5 - 7.5), streak-free polymers |
| Dermal Barrier & Safety Creams | Hydrolyzed Collagen, GHK-Cu Peptides, Tallow & Hyaluronic Matrix | Industrial occupational skin health, cleanroom hygiene, workshop care | Dermatologically tested, Non-comedogenic, Zero harsh sulfates | Viscosity tuning, airless pump packaging, private label branding |
Engineering Solutions for Australia's Harsh Operating Environments
1. Mining & Heavy Earthmoving (WA & QLD)
In the dust-heavy and extreme heat conditions of the Pilbara and Bowen Basin, heavy machinery accumulates tenacious red dirt, grease, and bitumen deposits. Our custom OEM quick-break solvent degreasers split oil from water in oil/water separators within minutes, ensuring Australian mining compliance and zero environmental runoff fines.
2. Food Processing & Abattoirs (VIC & NSW)
Australia’s agricultural export reputation demands flawless hygiene. We manufacture concentrated, fragrance-free quaternary ammonium compounds and chlorinated alkaline foamers tailored for high-pressure washdown in meat, dairy, and wine processing facilities, meeting rigorous HACCP standards.
3. Marine & Port Logistics (Fremantle & Brisbane)
Coastal logistics hubs require marine-grade salt-neutralizing washes and non-corrosive boat hull cleansers. Our formulation laboratory creates biodegradable, marine-safe surfactant complexes that effectively remove salt crusting, marine growth residues, and exhaust soot without harming marine biodiversity.
Unmatched Manufacturing Scale, Rigorous Quality Control & Australian Logistics Expertise
As a primary OEM contract manufacturer in China serving top Australian chemical importers and brand owners, we combine deep industrial chemistry expertise with flexible commercial terms. Our plant spans over 45,000 square meters, utilizing fully automated liquid synthesis reactors capable of producing over 150 metric tons of chemical formulations daily.
✓ Custom Formulation & R&D Flexibility
Our in-house R&D team comprises senior chemical engineers and cosmetic chemists. Whether you require modifying active solid percentages, adjusting foam heights, embedding anti-corrosion additives, or developing eco-friendly plant-based surfactant replacements, we formulate to your exact specification.
✓ Complete Private Label Packaging Solutions
We provide end-to-end packaging procurement and customization. From 500ml retail trigger bottles and 1L squeeze tubes to 5L industrial flagons, 200L L-ring HDPE drums, and 1000L UN-approved IBC totes—all fitted with fluorinated anti-collapse venting caps engineered for chemical ocean freight.
✓ Quality Control & Analytical Integrity
Every batch undergoes rigorous quality assurance including High-Performance Liquid Chromatography (HPLC), Viscometry testing, pH stabilization verification, accelerated thermal aging (45°C for 90 days), and freeze-thaw cycle testing to guarantee stability during trans-equatorial maritime shipping.
✓ Seamless Shipping to Major Australian Ports
Our dedicated export compliance team manages all customs documentation, Dangerous Goods (DG) declarations, packing group classifications, and FOB/CIF delivery straight to Sydney (Port Botany), Melbourne (Port of Melbourne), Brisbane, and Fremantle.
Frequently Asked Questions by Australian Importers & Distributors
Everything you need to know about custom compounding, AICIS regulatory compliance, MOQs, packaging, and ocean freight logistics to Australia.
Ready to Scale Your Chemical Brand in Australia?
Partner with China's top industrial cleaning chemicals OEM factory. Connect with our senior chemical engineering team today to discuss custom formulation, sample requests, and competitive FOB/CIF quotation.
Inquire Now