
Industrial & Commercial Manufacturing Portfolio
Explore our high-performance concentrate liquids, private label chemical lines, and specialized formulation capabilities tailored for international distributors.
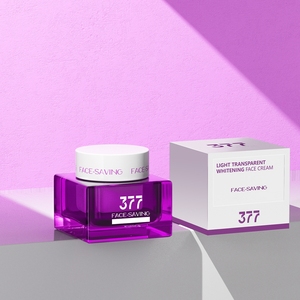
OEM Anti Aging Hydrolyzed Collagen Hyaluronic Acid Cream Arbutin Moisturizing Lightening Brightening Face Cream
Get Catalog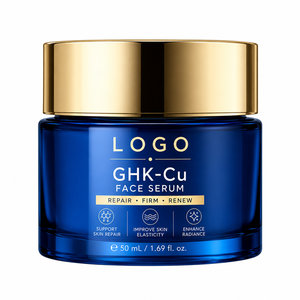
Private Label GHK-Cu Copper Peptide Face Cream Moisturizing Soothing Repair Anti-Wrinkle Firming Cream for All Skin Types OEM
Get Catalog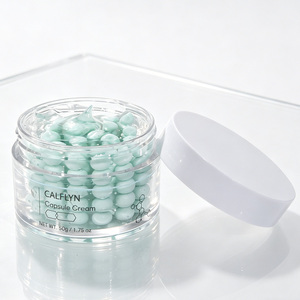
Capsule Pearl Ball Cream OEM ODM Private Label Collagen Anti-Aging Brightening Acne Control Hydrating Oil-Control Face Cream
Get Catalog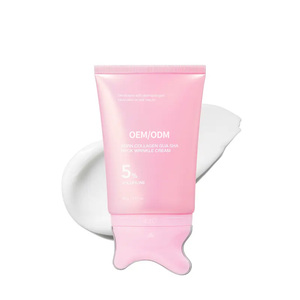
Private Label PDRN Collagen Gua Sha Neck Cream Cosmetic Tube Tighten Lift Neck Cream Volufiline 5 Anti Aging Wrinkle Cream 90g
Get Catalog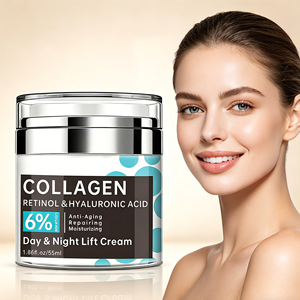
Private Label Collagen Retinol Hyaluronic Acid 7% Deep Moisture Nourishmen Science Proven Formula Cream Skin Care Face Cream
Get Catalog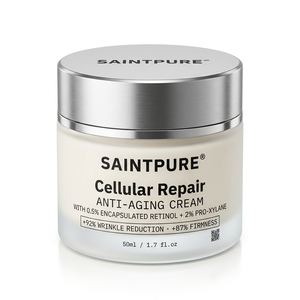
Private Label Anti-Aging Face Cream 50ml Encapsulated for Pro-Xylane Wrinkle Firming Cellular Repair Moisturizer OEM
Get Catalog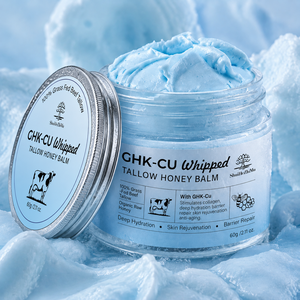
Private Label Copper Peptide GHK-Cu 100% Grass-Fed Beef Tallow Balm Deep Moisturizing Face Cream Anti-Aging Skin Repair OEM ODM
Get Catalog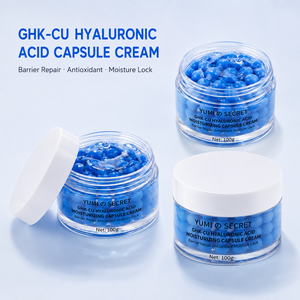
Private Label OEM GHK- Cu Copper Peptide Capsule Face Cream Anti Aging Firming Moisturizer for Mature Skin 100ml
Get CatalogEngineering & Sourcing OEM Floor Cleaner Concentrates: Strategic White Paper for Global B2B Buyers
In the modern commercial chemical manufacturing landscape, procurement managers and private-label distributors face escalating challenges regarding shipping logistics, volatile raw material costs, and stringent international environmental mandates. Partnering with a premier OEM Floor Cleaner Concentrate Factory & Supplier is no longer merely a transaction; it represents a strategic supply-chain optimization project that directly influences gross margins, operational safety, and sustainability scores.
Floor cleaner concentrates represent the pinnacle of liquid formulation efficiency. By stripping unnecessary water volume out of primary bulk manufacturing and focusing on high-density active surfactant matrices, commercial enterprises can reduce shipping freight volume by up to 80% while retaining superior soil emulsification and surface restoration properties. This white paper breaks down the chemical engineering standards, surface compatibility requirements, and regulatory benchmarks that define top-tier contract manufacturing.
High-Yield Dilution Ratios
Formulated for 1:100 up to 1:500 dilution rates. Designed to maximize operational coverage per drum for industrial scrubbers and manual sanitation systems.
pH Neutral Surface Safety
Advanced polymer chemistry engineered to safeguard marble, polished granite, epoxy resins, vinyl composition tile (VCT), and treated hardwood without residue build-up.
Eco-Surfactant Chemistry
Utilizing rapidly biodegradable Alkyl Polyglucosides (APG) and non-ionic surfactant bases compliant with European REACH and US EPA Safer Choice protocols.
Surfactant Matrix Engineering & Soil Emulsification Mechanics
The efficacy of a commercial floor cleaner concentrate relies on its micellar chemistry. Standard low-cost formulations rely heavily on sodium lauryl ether sulfate (SLES) or high-VOC solvent additives, which can leave dulling films, degrade floor waxes, or trigger health concerns in enclosed commercial spaces. Our in-house R&D laboratory designs custom formulation systems utilizing balance-optimized non-ionic and amphoteric surfactant blends.
Key technical parameters integrated into our contract manufacturing process include:
- Dynamic Surface Tension Reduction: Lowering liquid surface tension to under 30 mN/m allows rapid wetting across microporous ceramic tiles and porous natural stone.
- Controlled Foaming Characteristics: Engineered low-foaming profiles essential for automatic floor scrubbing machines, preventing vacuum motor damage and reducing rinse cycle water consumption.
- Chelating & Water Softening Complexation: Incorporating green chelating agents like GLDA (Tetrasodium Glutamate Diacetate) to neutralize hard water minerals (calcium and magnesium) without using phosphate builders.
- Quick-Drying Polymer Technology: Synthetic alcohol-free drying agents that accelerate evaporation rate while leaving a streak-free, anti-static slip-resistant surface.
Freight Economics & Supply Chain Sustainability Impact
Transporting pre-diluted cleaning solutions (which comprise 90% to 95% tap water) globally is economically inefficient and generates unnecessary carbon emissions. By procuring ultra-concentrated floor cleaning solutions from a centralized export-grade manufacturing hub in Malaysia, brand owners achieve substantial cost savings across the procurement cycle:
1. Volumetric Shipping Reductions: A single 200L drum of 1:200 floor cleaner concentrate replaces 40,000 Liters of ready-to-use product, dramatically slashing sea freight container requirements.
2. Packaging Waste Reduction: Concentrated formulas reduce primary plastic usage (HDPE bottles) by up to 75%, helping brands comply with corporate Extended Producer Responsibility (EPR) requirements.
3. Operational Warehousing Yield: Storage requirements in distribution centers are minimized, allowing inventory managers to double stock throughput without expanding physical footprints.
Future Sourcing Trends in Commercial Floor Care (2025–2030)
As commercial facility management, healthcare environments, hospitality chains, and retail networks adjust to stringent global hygiene standards, the demand for contract-manufactured cleaning solutions is undergoing rapid structural evolution. B2B buyers must align with OEM manufacturers who anticipate these major trends:
1. Enzymatic & Bio-Augmented Surface Care
Traditional chemical degreasers are increasingly being supplemented or replaced by active enzyme floor concentrates. These biological formulas utilize non-pathogenic bacterial spores that digest organic grease, starches, and fatty deposits inside grout lines long after the surface has dried. Ideal for commercial kitchens, food processing plants, and high-traffic restrooms.
2. Zero-VOC & Allergen-Free Formulations
Indoor Air Quality (IAQ) regulations in North America and Europe are setting strict limits on Volatile Organic Compounds. Next-generation OEM floor cleaners eliminate glycol ethers, synthetic terpenes, and artificial dyes, substituting plant-derived solubilizers and hypoallergenic scents that achieve LEED certification compatibility for green buildings.
3. Closed-Loop Dosing & Pod Concentrates
To eliminate manual dosing errors and operator exposure, commercial clients are transitioning toward automated wall-mounted proportioning systems and water-soluble concentrate pods. Contract manufacturers offering precise viscosity-controlled liquid dosing liquids gain a significant competitive advantage in institutional tenders.
4. Certified Halal & Ethical Industrial Hygiene
With the global expansion of Halal-compliant manufacturing in Southeast Asia and the Middle East, commercial hygiene products used in food processing facilities must carry authentic Halal certification. Our manufacturing lines guarantee zero cross-contamination with animal-derived ingredients or prohibited alcohol residues.
Enterprise OEM/ODM Advantages & Manufacturing Excellence
Operating out of state-of-the-art facilities in Malaysia, our company serves as a premier, GMP-certified, export-ready contract manufacturer trusted by international cosmetic, personal care, and industrial chemical brands. We combine deep chemical engineering expertise, rigorous quality control systems, and responsive account management to protect your brand reputation.
Stringent Compliance
Fully compliant with GMP (Good Manufacturing Practice), ISO Standards, NPRA regulations, and JAKIM Halal protocols, ensuring seamless import approval across global customs checkpoints.
In-House R&D Lab
Our dedicated R&D chemists possess access to over 500+ proven formulas, providing custom fragrance matching, accelerated stability testing, and target viscosity adjustment.
Flexible Packaging & MOQ
From 1L retail squeeze bottles and 5L commercial jerrycans to 200L HDPE drums and 1000L IBC Totes—we accommodate both growing startup brands and high-volume institutional contracts.
Frequently Asked Procurement Questions
Q1: What is the standard minimum order quantity (MOQ) for custom OEM floor cleaner concentrates?
Our standard MOQ for private label liquid concentrate formulations starts at 1,000 Liters for standard scents and formulations. For custom color matching, proprietary fragrance development, or specialized active ingredient complexing, MOQ typically ranges from 3,000 to 5,000 Liters per batch run.
Q2: Can your factory formulate pH-neutral concentrates for delicate marble and hardwood flooring?
Yes. We specialize in pH-neutral (pH 7.0–7.5) surfactant concentrates designed specifically for polished marble, terrazzo, natural granite, and sealed hardwood. These formulas effectively lift dirt without stripping protective sealant coats or dulling high-gloss finishes.
Q3: What international compliance documentation do you provide for bulk chemical export?
We provide comprehensive export dossiers including GHS-compliant Safety Data Sheets (SDS/MSDS in 16-section format), Certificates of Analysis (COA), Technical Data Sheets (TDS), Stability Testing Reports, Halal Certification, and Certificates of Origin (Form E/Form D) for tariff reductions.
Q4: How do you prevent ingredient separation or precipitation in high-concentration formulas during ocean freight transit?
All concentrate formulations undergo rigorous freeze-thaw cycle testing (-10°C to +50°C) and accelerated centrifuge testing to verify emulsion stability. We utilize advanced hydrotropes and polymeric stabilizers to guarantee a shelf life of 24 to 36 months under varying global storage conditions.
Q5: What packaging options are available for bulk commercial buyers versus retail private label clients?
We provide end-to-end packaging solutions: for retail and commercial supply chains, we offer 1L, 2L, and 5L HDPE containers with dosing caps or pump dispensers. For institutional and industrial buyers, we supply 200L L-ring HDPE drums and 1000L UN-rated IBC totes.
Q6: Are your floor cleaner formulas compatible with automatic scrubber machines?
Absolutely. Our commercial floor cleaner lines feature controlled low-foaming profiles specifically engineered for auto-scrubbers. This prevents foam overflow into recovery tanks, protects vacuum motors, and eliminates the need for expensive defoamer chemical additives.
Q7: Can we request eco-friendly, bio-based, or non-toxic chemical formulations?
Yes. We offer plant-derived surfactant matrices utilizing coconut oil and corn starch derivatives (APGs), enzyme-augmented grease digesters, and zero-VOC solvent substitutes. These formulas meet stringent eco-labeling standards worldwide.
Q8: What is the typical lead time from formula approval to finished shipment?
Once sample formulation and artwork are finalized, standard production and packaging lead times are 3 to 4 weeks. For re-orders of established formulations, turn-around times can be compressed to 10–14 business days.