
Featured Contract Packaged Formulations & Active Creams
OEM Anti Aging Hydrolyzed Collagen Hyaluronic Acid Cream Arbutin Brightening Face Cream
Get Catalog
Private Label GHK-Cu Copper Peptide Face Cream Moisturizing Soothing Repair Cream OEM
Get Catalog
Capsule Pearl Ball Cream OEM ODM Private Label Collagen Brightening Hydrating Face Cream
Get Catalog
Private Label PDRN Collagen Gua Sha Neck Cream Cosmetic Tube Volufiline 5 Anti Aging 90g
Get Catalog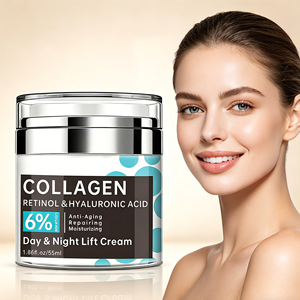
Private Label Collagen Retinol Hyaluronic Acid 7% Deep Moisture Nourishment Face Cream
Get Catalog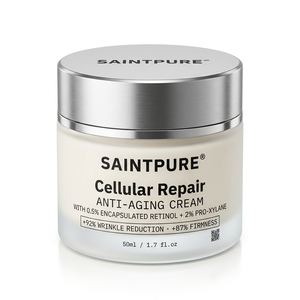
Private Label Anti-Aging Face Cream 50ml Encapsulated Pro-Xylane Cellular Repair OEM
Get Catalog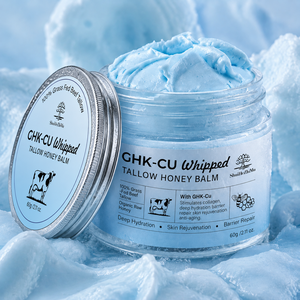
Private Label Copper Peptide GHK-Cu 100% Grass-Fed Beef Tallow Balm Deep Moisturizing OEM
Get Catalog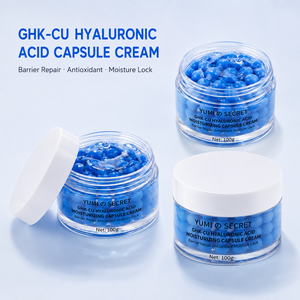
Private Label OEM GHK-Cu Copper Peptide Capsule Face Cream Anti Aging Moisturizer 100ml
Get CatalogIndustrial Competence & Infrastructure
Why leading global health, supplement, and skin-cosmeceutical brands choose our China & South East Asia contract manufacturing and packaging ecosystem.
High-Barrier Blister & Encapsulation
State-of-the-art thermoforming ALU-ALU and PVC/PVDC packaging lines ensuring extended shelf life, humidity resistance, and compound stability for sensitive actives.
Global Regulatory Compliance
Full regulatory documentation support including COA, MSDS, Halal, NPRA, ISO 22716, and FDA cGMP export readiness for frictionless cross-border distribution.
Micro-Encapsulation Active Tech
Pioneering delivery mechanisms such as pearl cream sphere encapsulation, PDRN stabilization, and GHK-Cu copper peptide preservation for maximum efficacy.
1. Executive Industry Insight: The Evolution of China Contract Supplement Packaging & Cosmeceutical Manufacturing
The global health supplement and advanced skin-cosmeceutical landscape is undergoing a structural paradigm shift. Driven by heightened consumer scrutiny, strict regulatory oversight, and a demand for biologically active formulations, brand owners can no longer rely on standardized, off-the-shelf contract manufacturing. Securing a competitive advantage in today's market requires partnering with specialized Top China Contract Supplement Packaging Manufacturers & OEM/ODM entities capable of integrating biomedical R&D with advanced high-barrier packaging engineering.
Contract packaging (often referred to as co-packing) is no longer a secondary downstream process; it is a vital pillar of product integrity, active potency preservation, and brand positioning. Modern nutritional supplements—ranging from sensitive hydrolyzed collagen peptides, probiotic micro-pellets, to botanical lipids—alongside advanced topical cosmeceuticals incorporating GHK-Cu Copper Peptides, Pro-Xylane, and PDRN (Polydeoxyribonucleotide), demand specialized packaging environments. Factors such as photo-degradation, oxidative stress, moisture vapor transmission rates (MVTR), and volatile compound migration must be precisely controlled through intelligent structural design and cleanroom manufacturing environments.
Our comprehensive contract packaging and manufacturing ecosystem bridges the gap between complex biochemical formulation and scalable commercialization. Operating under strict ISO 22716 and GMP protocols, we provide end-to-end turnkey solutions engineered for international brand owners, private label distributors, and enterprise wellness lines scaling across North America, Europe, the Middle East, and Southeast Asia.
2. Technical Analysis: Core Packaging Formats & Bio-Shielding Technologies
Selecting the appropriate packaging delivery vehicle is directly linked to active compound bio-efficacy and product shelf-life extension. Below is an engineering overview of the primary contract supplement and cosmeceutical packaging formats produced within our facility:
| Packaging Format | Primary Target Formulations | Barrier / Shielding Specs | Key Market Advantage |
|---|---|---|---|
| Cold-Form ALU-ALU Blister Packaging | Effervescent tablets, moisture-sensitive dietary capsules, hygroscopic botanicals | Zero MVTR, 100% Light & Oxygen Occlusion | Maximum active ingredient shelf stability up to 36 months without chemical preservatives. |
| Multi-Layer Airless Pump Dispensing | Copper Peptide GHK-Cu emulsions, Pro-Xylane serums, Retinol & Hyaluronic creams | Vacuum sealed, zero metallic reactivity, multi-layer PP/PETG | Prevents active oxidation; ensures precise dose metering with 99% container evacuation. |
| Dual-Chamber & Capsule Spheric Bead Jars | Collagen pearl balls, micro-encapsulated active suspensions, dual phase serums | Hermetic bead isolation within moisturizing hydrogel vehicle | Delivers fresh active release upon consumer application; high visual consumer engagement. |
| Cosmetic Squeeze Tubes with Integrated Applicators | PDRN neck creams, Gua Sha contouring gels, targeted eye repair serums | 5-layer EVOH high barrier tube with medical-grade zinc alloy massage heads | Combines topical formula delivery with mechanical physical therapy; premium user experience. |
| PCR Eco-Conscious Tallow & Balm Tins | Grass-Fed Beef Tallow balms, anhydrous bio-repair salves, lipophilic vitamin ointments | Recyclable tinplate / aluminum with food-grade internal lacquer lining | Aligns with global sustainability mandates while retaining lipophilic aroma and moisture. |
2.1 High-Barrier Material Engineering
For oral dietary supplements (nutraceuticals) and topical peptide creams, environmental exposure can degrade active potency within weeks if stored in standard low-density polyethylene (LDPE) or unshielded clear packaging. Our manufacturing facility employs advanced material science, including:
- EVOH (Ethylene Vinyl Alcohol Copolymer) Co-extrusion: Utilized in our tube packaging to create an imperceptible 5-layer gas barrier that prevents oxygen penetration and retains delicate essential aroma profiles.
- Amber UV-Absorbing Borosilicate Glass & PETG: Formulated with specialized UV-blocking additives that filter out destructive light wavelengths between 290nm and 450nm, protecting active light-sensitive molecules like Retinol, Arbutin, and Vitamin C derivative complexes.
- Desiccant-Integrated Closure Systems: Designed for solid dosage dietary supplement bottles, featuring molecular sieve desiccants built into the cap lid to maintain relative internal humidity below 20%.
3. Enterprise Strengths & In-House Manufacturing Capabilities
As a premier contract packaging manufacturer in China, our operations are built upon technical precision, full traceability, and vertical integration. We operate over 25,000 square meters of modern industrial infrastructure designed specifically to meet international standards.
3.1 ISO Class 7 & Class 8 Cleanroom Operations
Contamination risk is zero-tolerated in our production environment. All primary filling, capsule packaging, blister sealing, and cream emulsification take place within certified Class 7 and Class 8 cleanrooms equipped with positive-pressure HEPA filtration systems, automated temperature-humidity controls, and strict gowning airlock protocols. This ensures that every batch meets microbiological safety limits mandated by international health authorities.
3.2 Advanced Analytical Testing Laboratory
Every batch of raw ingredient and finished packaged product undergoes rigorous quality control within our internal analytical testing laboratory. Our chemical engineers and quality assurance specialists leverage state-of-the-art instrumentation:
- HPLC (High-Performance Liquid Chromatography): Used to quantify active compound concentrations, such as GHK-Cu purity percentages, Collagen peptide molecular weight profiles, and Retinol potency.
- Microbiological Assay Chambers: Continuous monitoring for aerobic plate counts, yeast and mold, E. coli, Staphylococcus aureus, and Pseudomonas aeruginosa.
- Accelerated Thermal & Humidity Stability Testing: Storage testing at 40°C / 75% Relative Humidity for 6 months to simulate a 3-year commercial shelf-life under extreme global transit environments.
4. Strategic Procurement Trends: Contract Packaging Innovations (2025–2030)
Procurement directors, brand strategists, and supply chain managers must stay ahead of emerging market shifts. Based on global consumer data and industrial packaging evolution, we highlight the four major procurement trends shaping the contract supplement packaging industry:
4.1 Micro-Encapsulation & "Fresh-Activation" Packaging Formats
Consumers are increasingly skeptical of passive skincare creams and static dietary pills. The demand is shifting toward visual proof of freshness. Innovators are turning to single-dose suspended capsules, pearl ball hydrogels, and dual-chamber packaging where active concentrates (such as lyophilized PDRN powder or concentrated Copper Peptides) are kept physically separate from the hydrating base emulsion until the moment of activation by the consumer.
4.2 The Sustainable Clean-Beauty & Clean-Label Packaging Mandate
Global legislative bodies, particularly in the European Union and North America, are enforcing stringent packaging waste reduction targets. Contract manufacturers are rapidly replacing traditional single-use virgin plastics with Post-Consumer Recycled (PCR) resins, mono-material recyclable aluminum, and refillable inner-cartridge jar systems. Procurement teams leveraging PCR packaging reduce carbon footprint metrics while commanding higher retail price premiums.
4.3 Smart Packaging, Anti-Counterfeiting, and Serialization
Counterfeit supplements and luxury skincare creams pose significant brand equity risks. Modern contract packaging now incorporates smart serialization, including invisible UV watermarking, encrypted QR codes, and tamper-evident hologram seals integrated directly during the automated outer carton box packaging process. This enables end-consumers to verify product authenticity instantly on their smartphones while providing brand owners with real-time global supply chain tracking.
4.4 Agility, Low MOQ Pilot Batches, and Modular OEM Scaling
The era of forcing brand owners into 100,000-unit minimum order quantities (MOQs) for new SKU launches is vanishing. Leading OEM/ODM contract manufacturers are adopting modular, flexible high-speed automated lines that allow agile brand managers to execute market testing with small batch pilot runs (3,000 to 5,000 units) before seamlessly scaling into mass production runs of over 500,000 units.
5. Technical Formulation Focus: Next-Gen Actives in Contract Packaging
Our in-house R&D team continuously develops stable base formulations that seamlessly pair with optimized contract packaging. Below are key bio-actives currently leading demand among international brand buyers:
5.1 GHK-Cu (Tripeptide-1 Copper) & Peptide Complexes
GHK-Cu is a naturally occurring copper complex renowned for signal peptide cellular repair, collagen synthesis promotion, and anti-wrinkle skin remodeling. However, copper peptides are notoriously sensitive to oxidation and pH shifts. Our contract packaging solutions utilize nitrogen-purged airless pump bottles or hermetically sealed pearl capsules to prevent copper ion degradation, guaranteeing maximum bio-reactivity upon application.
5.2 PDRN (Polydeoxyribonucleotide) & Volufiline Integration
Originating from high-end dermatological clinics, PDRN extracted from salmon DNA accelerates tissue regeneration, matrix repair, and skin elasticity recovery. Combined with Volufiline—a lipid-replenishing botanical active—our PDRN neck and facial creams are paired with integrated Gua Sha metal alloy applicator tubes. This dual packaging-formulation approach enhances micro-circulation while ensuring hygienic, precise application.
5.3 Encapsulated Pro-Xylane & Retinol Synergies
Pro-Xylane stimulates Glycosaminoglycans (GAGs) synthesis to restore extracellular matrix density. By applying micro-encapsulation technology, we enclose Pro-Xylane and Retinol within lipid spheres, which are then packaged in light-impermeable airless containers. This shields the sensitive actives from light oxidation while ensuring slow-release skin penetration without irritation.
6. Frequently Asked Questions (FAQ) – Procurement & Technical OEM/ODM Guidance
Our standard MOQs depend on the packaging format and active formulation complexity. For private label stock formulas with standard packaging (jars, tubes, or bottles), MOQs start as low as 1,000 to 3,000 units. For fully customized formulation development and custom-molded high-barrier packaging, MOQs generally start at 5,000 to 10,000 units. We also offer flexible pilot run programs for strategic brand expansion.
We employ a comprehensive stability testing protocol adhering to ICH guidelines. Products undergo real-time stability, accelerated thermal testing (40°C / 75% RH), freeze-thaw cycle testing (-10°C to 45°C), and photostability testing. Additionally, we conduct compatibility studies between the internal formula and primary packaging materials to ensure zero chemical leaching or container degradation over the product's shelf life.
Yes, absolutely. We have extensive export experience supplying over 30 countries. Our regulatory affairs department provides complete documentation dossiers including Certificate of Analysis (COA), Safety Data Sheets (MSDS), Certificate of Free Sale (CFS), INCI ingredient compliance checklists, Halal certificates, and ISO 22716 / GMP compliance certificates required for FDA, CPNP, or NPRA product registrations.
For existing private label stock formulations with standard packaging, typical lead times are 2 to 3 weeks. For custom ODM projects requiring bespoke formula development, laboratory stability testing, and customized packaging printing/manufacturing, production lead times generally range between 4 to 6 weeks following artwork and sample approval.
Yes. We offer an extensive portfolio of sustainable packaging solutions including Post-Consumer Recycled plastics (30% to 100% PCR PE/PET), 100% infinitely recyclable aluminum tins and tubes, FSC-certified outer paper cartons, bio-based sugarcane tubes, and refillable inner pod container systems designed to drastically lower environmental impact.
We enforce strict legal IP protection protocols. Prior to any technical formula discussion or sample formulation development, we enter into binding Non-Disclosure and Non-Circumvention Agreements (NDAs). Custom proprietary formulas developed specifically for your brand remain 100% your exclusive intellectual property.
7. Strategic Partnership & Turnkey Execution Roadmap
Partnering with an established contract supplement packaging and manufacturing leader streamline your supply chain, lowers capital risk, and accelerates time-to-market. Our 5-stage strategic execution model ensures seamless product launch efficiency:
- Stage 1: Intent & Formulation Consultation: Defining target market demographics, regulatory requirements, active ingredient benchmarks, and price-point targets.
- Stage 2: R&D & Sample Prototype Engineering: Formulating laboratory samples, conducting sensory/texture optimization, and performing rapid primary packaging compatibility tests.
- Stage 3: Regulatory Dossier & Packaging Design Approval: Finalizing outer box artwork, structural die-lines, label compliance reviews, and generating pre-production physical proofs.
- Stage 4: Automated Cleanroom Manufacturing & Packaging: Mass emulsification/blending, high-speed automated bottle/blister filling, nitrogen purging, inline weight checks, and box over-wrapping.
- Stage 5: Quality Assurance Release & Global Logistics: Final QA microbiological and HPLC batch release, palletization, container loading, and customs documentation dispatch.
Accelerate Your Brand with Premier Contract Packaging
Connect with our senior biochemical engineering and packaging procurement team today to request custom samples, complete catalog listings, and detailed OEM/ODM volume pricing.