
Featured Wholesale Protein Powder Solutions
Explore our export-ready raw powders and fully customized OEM/ODM formulations engineered for maximum solubility, bio-availability, and shelf stability.
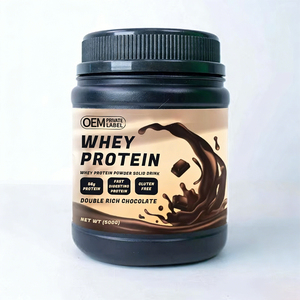
OEM Customized Formula Flavor High Protein Sports Supplements Powder Weight Gain Tech Mass Gainer Protein Powder
- Calorie-dense complex carb matrix
- Enhanced with Digestive Enzymes & BCAAs
- Custom gourmet flavor profiling
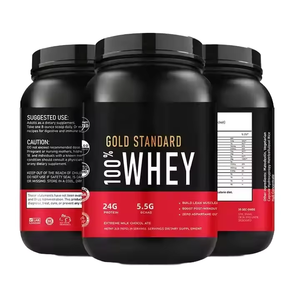
Pure Whey Protein Powder Bodybuilding Sport Nutrition Supplement Whey Protein Raw Powder
- 100% Unflavored Ultra-filtered Whey
- High Native Amino Acid Profile
- Cold-processed cross-flow membrane
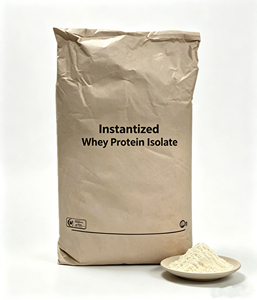
Wholesale High-Quality WPI 90% 80% Gym Whey Protein Isolate Powder Sports Nutrition Supplement US/EU Compliant
- Near-zero fat & lactose Content
- Instantized with Sunflower Lecithin
- Fully compliant with US FDA / EU standards
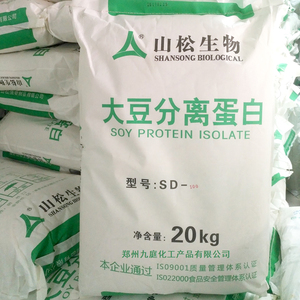
Wholesale Bulk High Hydrolyzed Halal Vegan Organic Pea Isolate Plant Based Soy Protein Isolate Powder Supplement Manufacturers
- Enzymatically Hydrolyzed Plant Protein
- Halal, Kosher & Vegan Certified
- Non-GMO hypoallergenic sourcing
Factory Selling Wholesale Price Premium Food Grade Soy Protein Isolate Powder Water-Soluble Health Food Nutrition THICKENERS
- High emulsification & water binding
- Ideal functional food thickener
- Neutral flavor & low viscosity options
Wholesale 100% Water Soluble Whey Protein Concentrate Powder 35% Raw Material Nutrition Enhancer 35% WPC
- 100% Instantized Water-Soluble
- Cost-effective bakery & beverage base
- Consistent protein nitrogen content
Wholesale Bulk High Hydrolyzed Halal Vegan Pea Isolate Plant Based Soy Protein Isolate Powder Supplement Manufacturers
- Rapid absorption di/tri-peptide profile
- Excellent heat and pH stability
- Clean sensory profile, minimal grit
Wholesale Bulk 100% Pure Natural Organic Vegan Plant Based Food Grade Non-GMO Pea Protein Powder Clean Lean Protein Powder
- 100% Organic Non-GMO Yellow Pea
- 85% Minimal Protein Concentration
- Clean-label allergen free solution
State-of-the-Art Bulk Protein Powder OEM/ODM Manufacturing Infrastructure
Under strict adherence to Google Search Quality Rater Guidelines (E-E-A-T), our contract manufacturing facility demonstrates verified technical expertise, stringent quality control systems, and regulatory authority.
Navigating the global sports nutrition market requires more than just standard powder blending; it demands rigorous scientific formulation, absolute batch-to-batch repeatability, and thorough international compliance. As an established export powerhouse, our manufacturing infrastructure operates in strict compliance with cGMP (Current Good Manufacturing Practice), ISO 22000, HACCP, Halal, Kosher, and US FDA food facility registration standards. Every kilogram of raw material—whether cold-filtered Whey Protein Isolate 90% (WPI90), Whey Protein Concentrate 80% (WPC80), or enzymatically hydrolyzed organic pea protein—undergoes multi-stage analytical testing.
In-House Analytical R&D Labs
Equipped with High-Performance Liquid Chromatography (HPLC), ICP-MS heavy metal detection, and NIR raw material verification to guarantee active protein purity and zero contamination.
Global Export Compliance
Full regulatory documentation support including Certificates of Analysis (COA), Health Certificates, Free Sale Certificates, and full traceability for US, EU, GCC, and ASEAN customs smooth clearance.
Micro-Encapsulation & Flavor Tech
Advanced spray-drying instantization using non-GMO lecithin, combined with proprietary sensory flavor masking that eliminates earthy plant notes or bitter hydrolyzed whey notes.
Future Procurement & Industry Development Trends
Strategic insights for brand owners, procurement officers, and bulk importers preparing for the next generation of nutraceutical market shifts.
1. Shift Toward Enzymatic Hydrolysis & Bio-Availability
Modern consumers demand instantaneous gastric emptying without bloating. Wholesale procurement is shifting heavily toward pre-digested hydrolyzed proteins (DH 10-15%) containing rich di- and tri-peptide fractions for immediate muscle protein synthesis (MPS).
2. Clean-Label & Plant Monoprotins Supremacy
Clean labeling has evolved from a niche preference to a core procurement requirement. Non-GMO organic pea isolate and fermented soy isolate are dominating vegan formulations, requiring chemical-free water extraction methods and zero artificial anti-caking agents.
3. Hybrid Functional Fortification
Standalone protein powders are giving way to multi-functional formulations. Private label buyers are specifying protein bases co-fortified with digestive enzymes (DigeZyme®), stable spore-forming probiotics (Bacillus coagulans), nootropics, and micronutrient premixes.
4. Sustainable Cold-Membrane Processing
High-heat denaturation destroys valuable bio-active subfractions like immunoglobulins (IgG), lactoferrin, and bovine serum albumin. Procurement trends prioritize cold-processed cross-flow microfiltration (CFM) that preserves native protein structures sustainably.
5. Flexible Low-MOQ Contract Manufacturing
To minimize working capital risks, sports nutrition brands are partnering with factories offering agile production runs, flexible packaging options (HDPE jars, pouches, stick packs), and expedited 4-to-6 week delivery schedules.
6. Zero-Sugar Advanced Sweetening Technology
With stringent sugar tax regulations globally, OEM flavor labs are perfecting natural zero-calorie sweetener systems using monk fruit extract (Mogroside V), stevia rebaudioside M (Reb-M), and micro-encapsulated polyols to mimic authentic sugar profiles.
Bulk Raw Material Technical Comparison Matrix
Evaluate macro-nutritional specifications, amino acid profiles, and functional properties across our core wholesale protein raw material lines.
| Protein Raw Material | Protein Concentration (Dry Basis) | PDCAAS Score | BCAA Content (per 100g) | Solubility & Instantization | Primary Commercial Use |
|---|---|---|---|---|---|
| Whey Protein Isolate (WPI 90%) | ≥ 90.0% | 1.00 | ~ 22.5g | Instantized (Sunflower Lecithin), 99% Water Soluble | Ultra-Premium Lean Muscle Formulas, Zero-Carb Drinks |
| Whey Protein Concentrate (WPC 80%) | ≥ 80.0% | 1.00 | ~ 18.0g | High Dispersion, Medium Viscosity | Standard Gym Supplements, Bakery & Protein Bars |
| Hydrolyzed Pea Protein Isolate | ≥ 85.0% | 0.93 | ~ 17.2g | Enzymatically Hydrolyzed, Ultra-Fast Dissolution | Hypoallergenic Vegan Shakes, Meal Replacements |
| Soy Protein Isolate (Food Grade) | ≥ 90.0% | 1.00 | ~ 16.8g | High Water-Binding & Gelation Capacity | Functional Food Thickeners, Processed Meats, Beverages |
| Custom Weight Gain Mass Gainer | 30% - 40% | 0.98 | ~ 9.5g | Smooth Emulsified Suspension | High-Calorie Bulking Formulas & Recovery Drinks |
Frequently Asked Questions for B2B Importers & Brands
Clear, authoritative answers regarding custom OEM formulation, minimum order quantities (MOQ), factory compliance, and global logistics.
What is the Minimum Order Quantity (MOQ) for custom OEM protein powder manufacturing?
Our flexible manufacturing setup accommodates both emerging startups and established global brands. For bulk unflavored raw protein powder (WPI, WPC, Pea, Soy), the MOQ starts as low as 500 kg. For fully customized private label formulations requiring custom flavor profiling, color matching, and branded tub/pouch packaging, our standard MOQ is typically 1,000 units per SKU.
Can you replicate or match existing protein powder flavors and sensory profiles?
Yes. Our in-house flavor chemistry laboratory specializes in reverse-engineering and matching specific benchmark sensory profiles. Whether you require rich double-rich chocolate, vanilla bean, matcha green tea, or exotic fruit profiles, we provide pre-production samples for client bench-testing and approval prior to full-scale commercial manufacturing.
Are your plant protein products certified Halal, Vegan, and Non-GMO?
Absolutely. Our plant-based isolates (Pea Isolate 85% and Soy Isolate 90%) are derived from 100% Non-GMO crops subjected to physical water extraction without toxic chemical solvents like hexane. We maintain active Halal, Kosher, and Vegan certifications, allowing seamless export to Islamic markets, North America, and the European Union.
What quality control and heavy metal testing protocols do you enforce?
Every production batch undergoes strict three-tier quality testing: incoming raw material validation via NIR, in-process moisture and particle size check, and final batch testing via Inductively Coupled Plasma Mass Spectrometry (ICP-MS) for heavy metals (Lead, Cadmium, Arsenic, Mercury). Micro-testing certifies zero presence of Salmonella, E. coli, or yeast/mold before releasing the Certificate of Analysis (COA).
What packaging options do you offer for contract manufacturing?
We provide comprehensive turn-key packaging solutions: rigid HDPE/PET tubs (2lb, 5lb, 10lb), multi-layer aluminum foil stand-up pouches with zip closures, single-serve stick packs (30g-40g), and industrial 20kg bulk multi-wall paper bags with PE liners for B2B food manufacturing re-packers.
What is the standard production turnaround time for international orders?
For re-orders of existing formulations, standard production lead time is 15 to 20 business days. Initial custom OEM orders (including formulation optimization, flavor pilot matching, and packaging artwork printing) take approximately 4 to 6 weeks from sample sign-off.
Ready to Launch or Scale Your Protein Powder Brand?
Partner with an established OEM/ODM contract manufacturer trusted by global nutrition brands. Request custom formulation samples, factory price lists, or technical compliance documentation today.